Laser or confocal: how to choose a distance sensor
Your target surface makes the decision, not the accuracy figure on the datasheet.

The most common specification mistake in distance measurement is choosing by accuracy. Two sensors quoted at the same micrometre figure can behave completely differently on your real part, because the datasheet number was measured on a matt ceramic reference surface — and your part is a polished shaft.
What triangulation actually measures
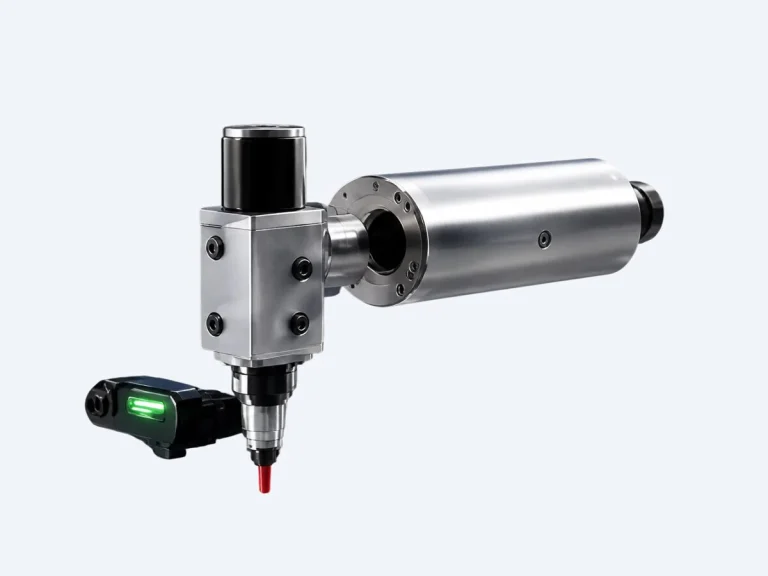
A triangulation sensor projects a spot of light and calculates distance from where the reflection lands on its detector. That needs a diffuse reflection. On a mirror finish the reflection goes somewhere else entirely, and the sensor either reads nothing or reads the wrong thing with complete confidence.
Where confocal takes over
Confocal chromatic sensors read the wavelength that comes into focus rather than the position of a spot, so a shiny surface is an advantage for them, not a problem. They also see both faces of a transparent layer at the same time, which is why glass thickness is a confocal application and not a triangulation one.
We test on the customer’s own samples before anyone commits to a sensor. It costs a week, and it has saved projects that would otherwise have failed at commissioning.
What matters besides the surface
The target surface is the first consideration, but not the only one. Three other figures sink a specification just as often:
- Working distance — how far the sensor can be kept from the part. In a hot or washdown cell this is decided before anything else.
- Spot size — a sensor whose measuring spot is wider than the feature you’re measuring will average it, not measure it.
- Measuring rate — see Matching measuring rate to line speed. A slow sensor on a fast line reports an average, not a dimension.
Full comparison table
| Property | Laser triangulation | Confocal chromatic |
|---|---|---|
| Mirror-like surface | Problematic — the reflection misses the detector | Excellent — the preferred working condition |
| Transparent material | Reads one surface only | Reads both surfaces at once |
| Typical working distance | 20 mm to 1000 mm | 2 mm to 60 mm |
| Measuring rate | Up to 49 kHz | Up to 70 kHz |
| Sensitivity to part angle | High | Low |
| Relative cost | Lower | Higher |
How to decide in practice
The practical route is a feasibility test on your material. Bring us the part; we’ll measure it with both technologies and send you the data.
What to bring to the test
One part in its production condition — not specially polished for the test — the measuring range you need, and the tolerance your process has to hold. Those three are enough to answer the question within a week.